TPU for Supercritical Foaming
Eleven grades tuned for physical foaming, from 60 Shore A soft-touch to 97 Shore A low-density high-hardness. Ester and ether backbones, plus a productivity-tuned HP series built for yield rather than a single property.
Physical properties
| Grade | Hardness | Density | Tensile | Elongation | Tear | Flame |
|---|---|---|---|---|---|---|
| NL1260L | 60A | 1.16 | — | — | — | — |
| NL1280L | 81A | 1.1 | — | — | — | — |
| NL9193A | 92A | 1.16 | — | — | — | — |
| NLDRS93A | 93A | 1.17 | — | — | — | — |
| NL9095 | 93A | 1.166 | — | — | — | — |
| NLLTE93A | 93A | 1.06 | — | — | — | — |
| NL9293A | 93A | 1.1 | — | — | — | — |
| NLHP93A | 93A | 1.06 | — | — | — | — |
| NL9393A | 94A | 1.14 | — | — | — | — |
| NLLTE97A | 96A | 1.11 | — | — | — | — |
| NLHP97A | 97A | 1.11 | — | — | — | — |
Complete specifications are per the official TDS — request the current technical data sheet.
What sets it apart
60 Shore A before foaming — the softest starting point in the line, for very low hardness after expansion.
Ester-based general-purpose foam grade: the widest processing window and the highest commercial maturity in the range. Start here unless you need a specific property.
High delamination tear — built for blend foaming and chemical foaming rather than straight SCF.
Low-melting polyether (LTE = low-temperature ether). Wide processing window at 1.06 g/cm³, useful when the foaming line runs cooler.
HP = high productivity. Tuned for yield: fewer rejects, wider processing range and better machine fit. The commercial argument, not the technical one.
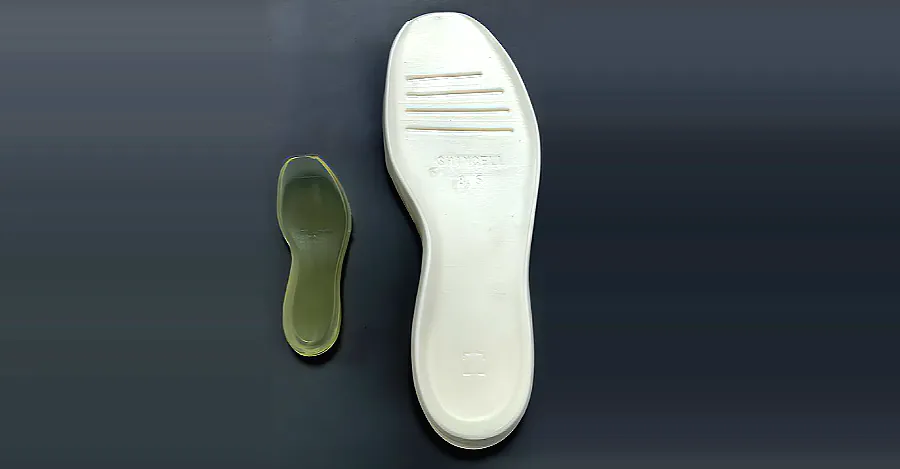
Low density combined with high resilience — the grade behind the 'small bead, large part' (小发大) moulding route.
Questions this line raises
Three answers that come up before a grade is chosen — deliberately short. The technical articles go deeper wherever the answer has a mechanism behind it.
What is supercritical foaming, and why does it need a different TPU?
Supercritical foaming uses CO₂ or N₂ above its critical point as the blowing agent instead of a chemical one. The gas dissolves into the melt under pressure and the cells form when the pressure drops, so the melt has to hold cell walls through expansion rather than rely on a decomposition reaction. That shifts what the grade must do: melt strength and crystallisation speed matter more than tensile strength, and the processing window narrows. Our foaming range — 60 to 97 Shore A, ester and ether backbones — is tuned for that, with an HP series tuned for yield at a given density.
Does a foamed part's hardness follow the grade's Shore A?
No. Once a part is foamed, the feel is set by density and cell structure, not by the durometer of the pellet: a 93 Shore A grade can be moulded into a soft midsole and a 60 Shore A grade into a firm one, depending on expansion ratio. That is why a foam grade is not selected on hardness alone. Specify what the finished part must do — density, resilience, compression set, tear — and treat the pellet hardness as a processing input that tells you how much expansion the melt will carry.
How do I choose a grade for a new part?
Start from four facts, not from a datasheet: what the part touches and for how long, how it is processed (injection, extrusion, film casting), the service temperature, and any standard the finished part must meet. Those four narrow the polyol chemistry and the hardness band; only then is the grade list short enough to compare. Bring those four to us and the answer is a specific grade rather than a range.